Premium grade bioactive bulk raw materials engineered for nutraceutical capsules, functional beverages, gut health formulas, and clinical wellness applications.

China Factory Directly Supply Food Grade Bulk Powder Mineral Premix Powder Food Ingredients 10% Folic Acid for Human Supplement
Explore Ingredient
Calcium Carbonate Bio Compatible Powder Mineral Supplement Material for Calcium Rich Formula and Nutrition Component Preparation
Explore Ingredient
Doking Hot Selling Quality OEM Fruit Flavored Bubble Tea Ingredients Milk Tea Materials Passion Fruit Compound Enzyme Drink
Explore Ingredient
16 Years Service Life Free Sample Sodium Polyacrylate Polymer In Chemicals Potassium Polyacrylate Super Absorbent Polymer SAP
Explore Ingredient
Wholesale New Technology Microneedling Kit PDRN Microcrystalline Cleansing Gel and Anti Wrinkle Serum Set Private Label
Explore Ingredient
OEM ODM High Protein Gummies Sugar Free For Muscle Growth & Beauty Energy Boost Strawberry Gummy Private Label Supplement 60pcs
Explore IngredientThe global digestive health sector has transitioned from simple, reactive constipation remedies to proactive, system-wide microbiome optimization. Modern gastrointestinal science validates that the human gut functions as the "second brain," governing metabolic homeostasis, systemic immunity, mood regulation via the gut-brain axis, and nutrient bio-availability. Consequently, global nutraceutical brand owners, pharmaceutical packagers, and functional beverage innovators demand sophisticated, multi-targeted raw ingredients from verified industrial manufacturing hubs.
China has solidified its position as the world's primary manufacturing nexus for advanced digestive health ingredients, combining rich botanical biodiversity with state-of-the-art precision bio-fermentation and chemical extraction infrastructure. Leading supply partners provide raw ingredients engineered to overcome historically persistent formulation challenges, such as gastric acid degradation, poor water solubility, heat instability during high-temperature processing, and undesirable organoleptic profiles.
Moving beyond live strain vulnerability, heat-stable heat-killed postbiotic lysates and short-chain fatty acid (SCFA) precursors offer unparalleled shelf stability while directly fortifying mucosal integrity and epithelial tight junctions.
High-potency fungal and plant-derived enzymes (such as high-activity Pectinase, Protease, and Amylase complexes) facilitate efficient macronutrient breakdown, alleviating bloating, malabsorption, and inflammatory responses in sensitive consumers.
Botanical concentrates rich in rare fatty acids (like Seabuckthorn Pulp Oil high in Omega-7) and concentrated polyphenols ( Bitter Melon, Mushroom Beta-Glucans) repair damaged gut linings and reduce systemic gut-induced inflammation.
The global trade architecture for digestive health ingredients has shifted dramatically toward vertical integration. Enterprise brand owners across North America, Western Europe, and Asia-Pacific are increasingly disintermediating legacy brokers to build direct, resilient relationships with top tier Chinese bio-manufacturing facilities. This strategy ensures strict supply security, full batch-level traceability, and direct technical collaboration during formulation development.
China's competitive moat in digestive health manufacturing is grounded in four structural advantages:
Chinese factories house massive multi-ton stainless steel bioreactors equipped with automated continuous-flow monitors, allowing for precise control of microbial cell densities, substrate conversion rates, and enzyme yields at economies of scale that cannot be matched regionally in overseas markets.
Direct integration with domestic agricultural regions ensures reliable access to raw botanicals—ranging from Seabuckthorn and Bitter Melon to medicinal mushrooms and traditional fermented bases. Supercritical CO2 and membrane filtration technologies retain delicate bio-actives without chemical solvent residues.
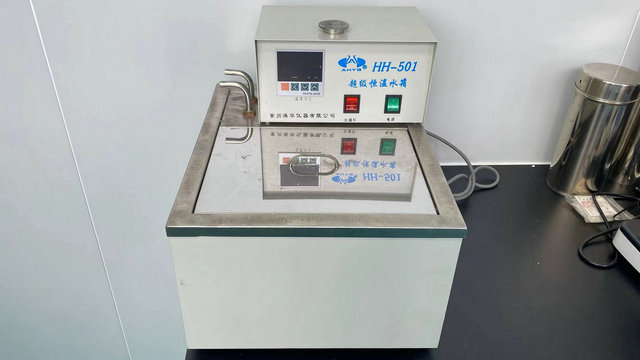
Premier Chinese suppliers operate ISO 17025 accredited testing laboratories featuring High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and Inductively Coupled Plasma Mass Spectrometry (ICP-MS) to guarantee zero heavy metal contamination and strict active compound standardized assays.
Leading Chinese manufacturers maintain dedicated international compliance units that prepare comprehensive Drug Master Files (DMF), US FDA GRAS notifications, EU Novel Food Dossiers, and fully localized customs documentations for seamless cross-border shipping.
Hangzhou Soy Extracts Co., Ltd. is a leading China dietary supplement ingredients manufacturer specializing in the research, development, production, and supply of high-quality nutraceutical raw materials for health and wellness products. With a strong commitment to innovation, quality, and sustainability, the company provides comprehensive ingredient solutions to dietary supplement brands, manufacturers, and distributors worldwide.
Leveraging advanced production technologies and modern manufacturing facilities, Hangzhou Soy Extracts offers an extensive portfolio of dietary supplement ingredients, including botanical extracts, plant proteins, amino acids, vitamins, minerals, functional ingredients, and other nutraceutical raw materials. These ingredients are widely used in dietary supplements, functional foods, sports nutrition products, health beverages, immune support formulations, and wellness applications.
Innovation is at the core of the company's business philosophy. Supported by a highly experienced R&D team, Hangzhou Soy Extracts continuously explores new ingredient technologies and formulation solutions to meet the evolving needs of the global nutraceutical market. The company also provides customized ingredient development and OEM/ODM support, helping customers accelerate product innovation and strengthen market competitiveness.
Quality assurance is integrated into every stage of production. From raw material sourcing and manufacturing to final inspection and packaging, strict quality control procedures are implemented to ensure product consistency, purity, safety, and compliance with international standards. The company is dedicated to delivering reliable and traceable ingredient solutions that meet the stringent requirements of global customers.
With customer satisfaction as its priority, competitive manufacturing capabilities, stable supply chains, and professional technical support, Hangzhou Soy Extracts Co., Ltd. has established long-term partnerships with clients across international markets. The company remains committed to providing premium nutraceutical ingredients that support healthier lifestyles and contribute to the sustainable development of the global health and wellness industry.
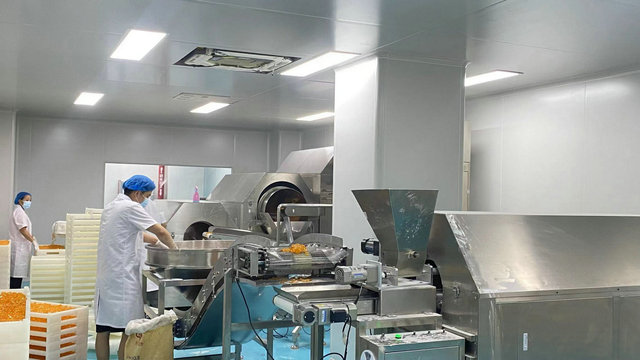
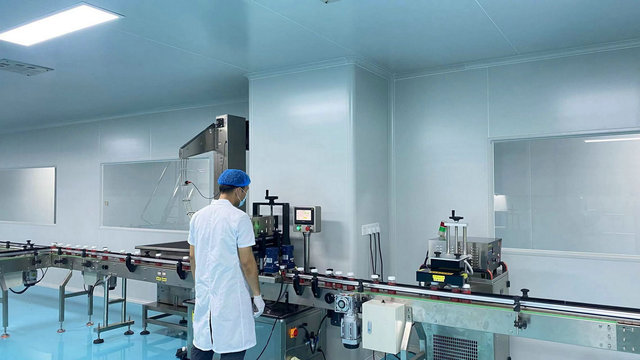
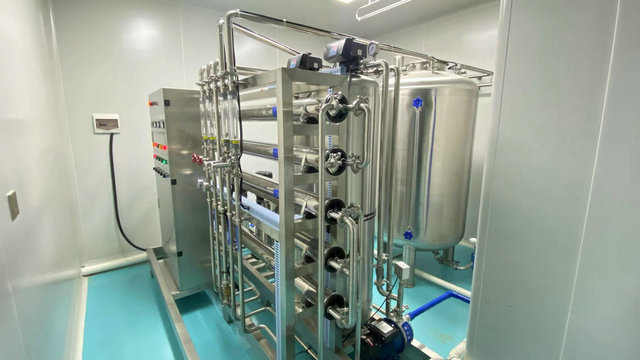
Direct glimpse into our state-of-the-art cleanroom production lines, quality assurance laboratories, and raw material storage systems.
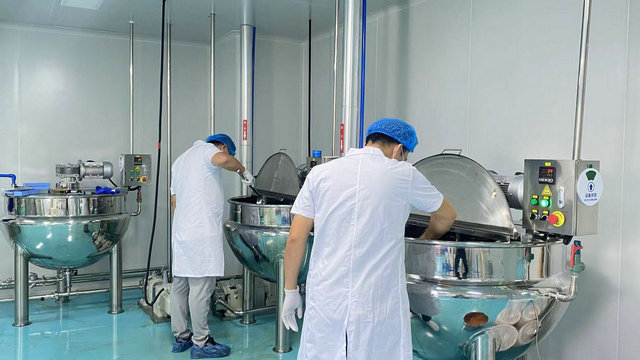
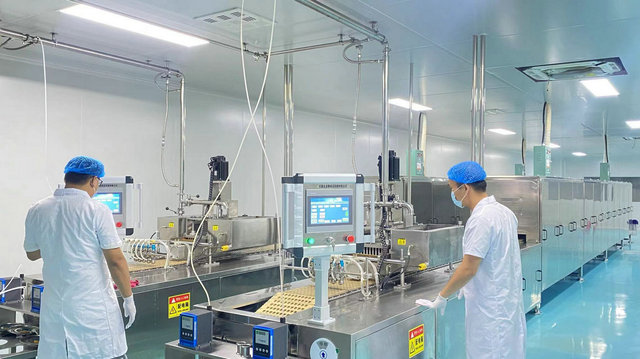
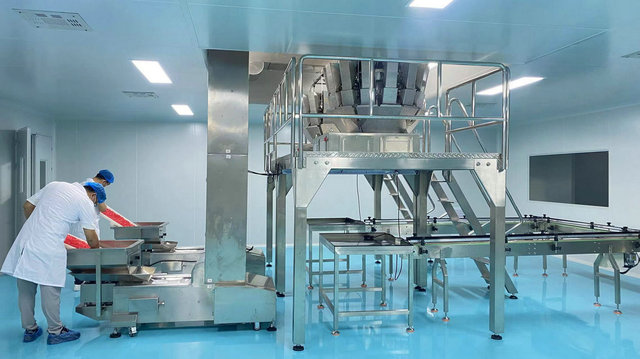
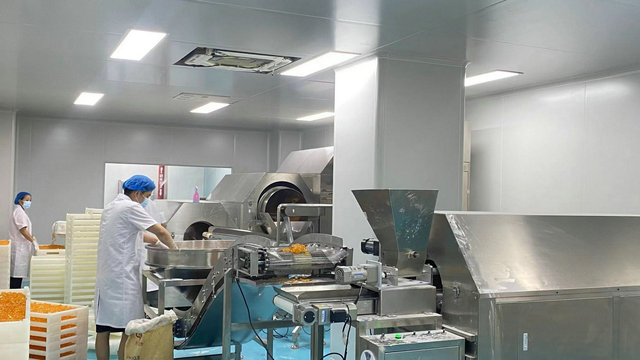
The industrial roadmap for digestive health ingredient synthesis over the 2025–2030 horizon is driven by advancements in synthetic biology, targeted release kinetics, and microbial strain bio-engineering. Key technological focus areas driving modern factory investments in China include:
| Technology Pillar | Technical Mechanism | Target Product Applications | Commercial Advantage |
|---|---|---|---|
| Microencapsulation & Liposomal Delivery | Lipid bilayer coating and ethylcellulose matrix shielding active molecules against stomach acid (pH 1.5–2.0). | Probiotics, Enzymes, Bitter Extracts, Folic Acid Premixes. | Increases intestinal bio-availability by up to 340%; eliminates bitter taste. |
| Precision Yeast Fermentation | Recombinant Saccharomyces cerevisiae strain engineering for sustainable protein and polysaccharide expression. | Yeast Protein Powder, Beta-Glucans, Postbiotic Peptides. | Zero reliance on animal agriculture, non-allergenic, ultra-pure protein profile. |
| Synbiotic Matrix Co-Crystallization | Dual-phase aggregation of specific prebiotic fibers with heat-treated probiotic bacterial lysates. | Gummies, Functional Instant Powders, Effervescent Tablets. | Synergistic gut microbiome colonization and zero thermal degradation during tableting. |
| Biomimetic Enzymatic Conversion | Recombinant enzyme cascades optimized via directed evolution for targeted plant cell-wall digestion. | Pectinase, Botanical Bio-actives, Silk Amino Acids. | Higher extraction yields, eco-friendly water extraction, lower carbon footprint. |
Modern consumers demand versatile delivery formats beyond traditional hard capsules and tablets. Factories must engineer raw materials to perform flawlessly across diverse food, beverage, and nutra-cosmetic matrices while maintaining sensory appeal and biochemical potency.
Engineered for thermal endurance. Ingredients such as sugar-free high protein matrices, Moringa Leaf Extract, and standardized vitamins withstand 90°C gummy depositor temperatures without degradation or texture alteration.
Instant cold-water soluble powders, fruit-flavored compound enzymes, and clarity-optimized pectinases allow liquid product developers to create clear, shelf-stable digestive tea tonics and sports recovery shots.
The gut-skin axis connects internal microflora balance with external skin elasticity and radiance. Ingredients like PDRN complexes, Seabuckthorn Pulp Oil (Omega-7), and Silk Amino Acids serve dual oral-dermal functional roles.
Navigating global regulatory landscapes requires meticulous analytical validation and localized technical support. Top tier China digestive health suppliers operate robust Quality Management Systems (QMS) aligned with tier-one international standards to simplify client audit processes and ensure friction-free customs clearance.
Every ingredient shipment is accompanied by batch-specific Certificates of Analysis (COA), Safety Data Sheets (SDS), Allergen Declarations, Non-GMO verification, BSE/TSE-free certification, and full origin traceability records required by FDA, EFSA, and TGA inspectors.
Manufacturing sites are fully certified under cGMP (Current Good Manufacturing Practice), ISO 22000, ISO 9001, HACCP, Halal, and Kosher protocols. Facilities undergo routine third-party audits by international bodies such as SGS, Intertek, and NSF.
From initial benchtop lab samples to commercial-scale batch trial runs, localized technical application teams assist overseas buyers with viscosity adjustment, taste masking, particle sizing (mesh optimization), and premix homogeneous blending.
Strategic safety stock holdings and partnerships with global freight forwarding networks enable reliable maritime and air cargo transportation with guaranteed lead times, vendor-managed inventory (VMI) arrangements, and flexible Incoterms (FOB, CIF, DDP).
Expert answers regarding ingredient sourcing, quality validation, minimum order quantities (MOQ), and contract manufacturing from China factories.
China offers unmatched scale, vertically integrated raw material supply chains, and significant bio-fermentation cost efficiencies without compromising quality. Advanced Chinese facilities operate under identical international cGMP standards and utilize the same high-end analytical equipment (Agilent, Shimadzu HPLC/GC-MS) found in Western laboratories, providing equivalent quality at a far more competitive unit price.
We enforce strict multi-stage quality control. Every batch undergoes raw material identity verification, in-process processing monitoring, and finished product assay testing for active compound content, heavy metals (Lead, Arsenic, Cadmium, Mercury), pesticide residues, microbial limits, and residual solvents. Full COA documentation accompanies every delivery.
Yes. Hangzhou Soy Extracts Co., Ltd. maintains dedicated cleanroom blending and encapsulation lines. We provide custom formulation, particle mesh customization (micronization), premix granulation, and private label OEM/ODM services for gummies, sachets, capsules, and functional beverage bases tailored to your brand’s specific market requirements.
Standard raw material orders are typically dispatched within 7–14 business days from our stock reservoirs. For custom bio-extract batches or OEM gummy orders, lead times range between 3 to 4 weeks. MOQs start as low as 1 kg to 25 kg for high-value bioactive extracts, while bulk food-grade minerals and yeast proteins typically carry an MOQ of 100 kg to 1,000 kg.
Absolutly. Our international regulatory team ensures that ingredients comply with FDA dietary supplement regulations (NDIN requirements), EU Novel Food directives, EFSA safety thresholds, and regional labeling guidelines. Complete technical dossiers are provided to simplify your brand's regulatory registration.
Enterprise buyers can contact our international sales office directly through our website product links or inquiry forms. Free pre-production testing samples (100g – 500g) complete with lot-specific COAs are dispatched via DHL/FedEx priority courier within 48 hours for laboratory evaluation and benchtop testing.
Explore our extended range of bio-active extracts, amino acids, enzymes, and functional health materials manufactured to high global standards.

China Manufacturer Wholesale OEM Private Label Vegan 200mg Moringa Leaf Extract Gummy Supplement For Antioxidant
Explore Ingredient
Factory Manufactured Herbal Ingredients for High Purity Bitter Melon Extract Powder
Explore Ingredient
6 In 1 Mushroom Extract Blend Powder 30% Beta Glucan With Matcha & Pine Pollen Raw Material
Explore Ingredient
Unflavored Fish Gelatin Food Grade Marine Gelatin Powder Food Grade Gelatin Gelatin Capsule Shells Gelatin Powder
Explore Ingredient
Food Grade Yeast Proteinfood Supplement Gradenutrition Yeast Protein Powder High Grade Thickeners
Explore Ingredient Soy Extracts